Vertical Lift Rack Zinc Plating Equipment Factory: Essential Guide to Choosing the Right Partner
2026-11-16
Choosing the right partner for vertical lift rack zinc plating equipment can make or break your production line—poor plating quality, frequent downtime, and hidden costs are just the beginning. In this guide, we cut through the noise with practical insights on what truly matters, from tank design to automation. Whether you're upgrading or building from scratch, Junda brings decades of hands-on expertise to help you avoid costly mistakes and get it right the first time.
How Vertical Lift Rack Design Dictates Plating Uniformity
The geometry of a vertical lift rack isn't just a structural afterthought—it directly governs how current reaches every part in the bath. When parts hang at fixed angles or are densely packed on center rods, the electrical field bends around edges and shadows recessed areas. A rack with uneven spacing or too many contact points creates hot spots where plating builds thick, while shielded zones stay thin or even skip entirely. Designers who ignore this end up with parts that look fine on the outside but fail on dimensional checks.
One overlooked factor is the way the rack's vertical movement introduces a changing immersion profile during entry and exit. If the rack tilts or sways because of poor frame rigidity, parts near the bottom linger longer in the high-current zone, while those at the top get a shorter dwell time. Over hundreds of cycles, that discrepancy compounds, producing batch-to-batch variation that no amount of rectifier tweaking can fix. A well-engineered rack keeps every part traveling through the same plating thickness contour.
Practical fixes involve more than just adding extra contacts. Adjusting the rack's pitch, using auxiliary anodes for deep recesses, and trimming unused hooks all reduce stray current paths. Even the choice of plastisol coating thickness on the frame changes the local voltage drop, which in turn alters deposit distribution. The best plating lines treat rack design as part of the process recipe, not as a one-time setup task.
The Factory Visit Checklist Most Buyers Skip
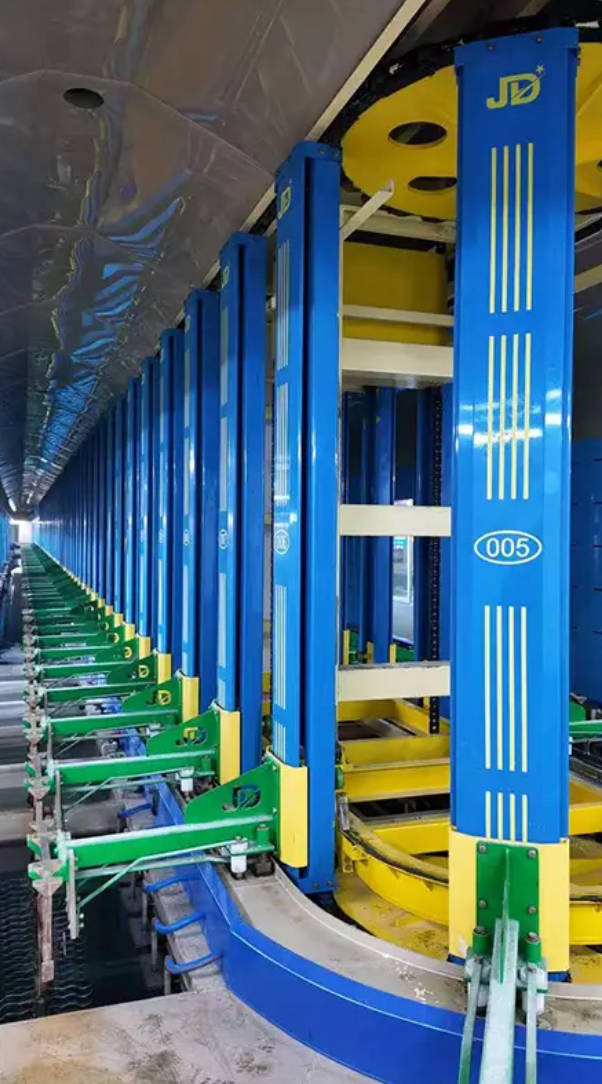
Walking through a factory, most buyers fix their eyes on the production line and the sample room, checking whether the machines look busy and the finished goods match the approved specs. But the real story often hides in the raw material warehouse. Look at how incoming materials are stacked, whether lot numbers and arrival dates are clearly marked, and how often the inventory records are updated. A warehouse where boxes are piled haphazardly or where the same batch sits untouched for months suggests poor planning, cash flow problems, or both—none of which bode well for your future orders.
Another blind spot is the equipment maintenance log. Factories routinely wipe down machines and sweep floors before a visitor arrives, but the logbook rarely lies. Flip through the pages and check the intervals between service dates, the types of repairs recorded, and whether any parts were sourced from outside suppliers. Long gaps or repeated fixes on the same component indicate that the machinery is being run into the ground, and breakdowns will likely interrupt your production schedule. Pay attention, too, to how quality inspectors interact with line workers—if defects are quietly set aside instead of discussed openly, the factory's real rejection rate is probably much higher than what you're told.
One more detail that nearly everyone overlooks: where the rejects and scrap go. Walk behind the main building and see how waste is handled. A well-run factory separates metal shavings, plastic trimmings, and defective parts into labeled bins, with a clear schedule for recycling or disposal. If you find scrap piled in corners, mixed with household trash, or being fed back into the raw material stream without any sorting, treat it as a red flag. It signals weak process control, cost-cutting shortcuts, and a management style that tolerates sloppiness—conditions that will eventually surface in your own products.
Material Specs That Separate a 10-Year Tank from a 3-Year Tank
The difference between a tank that survives a decade and one that fails in three years often comes down to the metal recipe and the welding process behind it. Cheap tanks use thin-gauge carbon steel with minimal corrosion allowance, which rusts through once the protective lining scratches. High-endurance tanks switch to duplex stainless or add a sacrificial anode layer, pushing the wall thickness past what standard pressure cycles demand.
Look at the seam where the bottom meets the shell. A three-year tank typically uses a single-pass weld, leaving micro-pores that trap moisture and accelerate pitting. A ten-year tank goes with a double-sided, full-penetration weld, then shot-blasts the joint and applies a 300-micron epoxy coating inside and out. That extra step costs a few dollars at the factory but changes the failure mode from sudden leak to slow, scheduled replacement.
Certification labels hide the real spec. Instead of trusting the logo, demand the actual material certificate: minimum yield strength above 345 MPa, elongation over 20%, and a documented NACE MR0175 compliance if any sour gas is present. Tanks built to those numbers rarely die from wall loss. They get retired because the fittings wear out first.
Automation Without the Headaches: What to Demand from Controls
Real automation headaches rarely stem from the machinery itself. They come from control systems that bury fault details in ladder logic, lock you into a single vendor's programming cable, or force a full line shutdown just to change a timer preset. Demand controls that surface diagnostics in plain language—something a shift technician can read without opening the engineering suite. Ask what happens when a photoeye goes intermittent or a drive throws an overcurrent at 2 A.M. If the answer doesn't include a clear, remote-readable alarm with a suggested cause, keep looking.
Interoperability is the second non-negotiable. A control should expose every tag, alarm, and setpoint over open protocols like EtherNet/IP, PROFINET, or OPC UA without needing a proprietary gateway or a $400-per-seat viewer. If your SCADA or MES can't pull a temperature setpoint today, you're not buying automation; you're buying a future integration project with interest. Demand offline simulation too—you should be able to test logic changes on a laptop, not on a running production line.
Finally, demand version discipline. Controls that silently auto-update firmware, rename tags between revisions, or require matching software versions across three different packages are the real source of 3 A.M. calls. Insist on a clear change log, backward-compatible tag naming, and a documented rollback path. The right control system shouldn't feel like a black box; it should feel like a tool you can trust when the line is down and the order is late.
After the Sale: Testing a Supplier’s Real Support Muscle
Most buyers get spoiled by a sales rep's rapid replies before the deal closes. But the real test comes when a machine goes down at 2 a.m. or a critical part fails without warning. If a supplier takes days to answer an email after the invoice is paid, or routes every technical question to a junior call center, their support promise is just paper. Smart procurement managers plant a few test clauses in the contract: demand a 24-hour on-site diagnostic for a simulated fault, or trigger an urgent spare parts request just to see how quickly the supplier's distribution network actually moves.
Another detail that gets overlooked is documentation and training. Many suppliers ship a PDF manual and call it a day, but no one trains the line operators who will use the equipment daily. A supplier with real support muscle sends an engineer to the floor, logs abnormal behavior during the first weeks of operation, and leaves behind a preventive maintenance calendar tailored to your shift patterns. These moves don't generate immediate revenue, but they quietly cut hidden costs over the second half of the equipment's life.
Finally, ask this blunt question: what happens if you discontinue this model next year? Some suppliers only support current production lines. Once a product is revised, old-model spare parts and software updates disappear. A simple test is to request a five-year spare parts availability record for a discontinued product, plus a written commitment to keep supplying parts for your unit for the next five years. Suppliers willing to share that kind of history and sign that kind of promise are the ones that actually take after-sale support seriously.
Total Cost of Ownership: Beyond the Initial Quote
A lot of purchasing decisions get made on the basis of the upfront quote, but that number rarely reflects what you will actually spend over the life of the product or service. Things like routine maintenance, energy use, replacement parts, training time, and even downtime during repairs start adding up once the purchase is complete. In many cases, these ongoing costs are far larger than the original price tag—especially for equipment or software that needs constant support or has a steep learning curve.
Before committing to a quote, it helps to think through the full ownership timeline. Ask about expected lifespan, warranty coverage, upgrade paths, and what happens when something breaks outside of normal hours. Comparing options only makes sense if you include projected running costs over the same period. Sometimes a higher initial price comes with lower long-term expenses, so the cheapest quote can end up being the most expensive choice by year two or three.
FAQ
Pay attention to the factory's floor experience, especially with automated rack handling and zinc bath agitation. Ask for detailed drawings and past installations in similar industries. A reliable partner will show you how they prevent rack swing and uneven coating before you sign anything.
It is often the difference between smooth production and constant downtime. Look for a lift that offers controlled acceleration and deceleration, corrosion-resistant guides, and easy access for maintenance. Cheaper designs may save upfront but lead to more rejects from drips or misalignment.
Instead of general questions, ask about bath temperature control, anode placement, and how the equipment handles hydrogen embrittlement risk for high-strength parts. A factory that can discuss these details without vague answers usually has real process knowledge.
Not necessarily. A smaller factory with focused expertise in rack plating can outperform a larger generalist. The key is whether they have built similar lines recently and can provide references from plants running comparable part sizes and volumes.
Ask for a full equipment layout, utilities consumption, cycle time calculation, and a clear scope of supply. If they are hesitant to provide these early, it may indicate hidden gaps in engineering or project management.
Request a typical spare parts list with lead times, and ask how they handle emergency breakdowns after installation. A good factory will have standard modular components and offer remote diagnostics or on-site support within a defined timeframe.
Avoid simply choosing the lowest price. Compare what is included in each quote: rectifiers, ventilation, controls, safety features, and installation supervision. An itemized quote makes it easier to see where one supplier may be cutting corners.
Conclusion
Choosing a vertical lift rack zinc plating equipment factory goes far beyond comparing brochures. The rack design itself sets the ceiling for plating uniformity—how workpieces are hung, current distribution across the rack, and the lift stroke directly determine whether corners plate evenly or build up excessive thickness. Before signing anything, walk the shop floor with a checklist most buyers overlook: watch a loaded rack cycle through the line, ask about anode placement and agitation, and inspect welds on racks that have seen real production. A factory that hesitates to show you live operations is telling you something.
Material choices separate equipment meant to last ten years from tanks that rust through in three. Ask for mill certificates, not just verbal assurances—polypropylene thickness, frame steel grade, and fastener materials matter. On controls, insist on automation that operators can actually use: recipe storage, fault logging, and manual overrides that don't require an engineer on speed dial. Real support reveals itself after commissioning; probe how the factory handles emergency parts, remote diagnostics, and training turnover when your maintenance crew changes. Finally, run a total cost of ownership model covering rectifier efficiency, chemical drag-out, replacement part lead times, and downtime risk. A low initial quote often hides expensive shortcuts in exactly these places.
Contact Us
Contact Person: hayyr
Email: [email protected]
Tel/WhatsApp: 8613082110525
Website: https://www.jundaelectroplating.com