Best Breathable Membrane Manufacturer: Ensuring Optimal Performance and Durability
2026-07-24
When it comes to protecting buildings from moisture while allowing vapor to escape, the choice of breathable membrane can make or break a project. As the demand for high-performance building materials soars, Jinbo stands out as a manufacturer that goes beyond the basics. In this post, we'll explore what sets Jinbo apart in the quest for optimal performance and durability—and why it matters for your next build.
Superior Breathability for Enhanced Product Longevity
When materials can breathe, they naturally resist the buildup of moisture and heat—two silent killers of durability. This product is engineered with a structure that allows continuous air exchange, preventing the damp, stagnant conditions that accelerate wear and tear. By staying dry and cool, the physical integrity is preserved far longer than conventional alternatives.
The design uses microscopic venting channels that actively wick away humidity while blocking external particles. It’s not just about passive airflow; it’s a dynamic system that adapts to changing conditions, keeping internal components at an optimal state. This reduces the expansion and contraction cycles that so often lead to cracking, warping, or delamination.
In practice, that means fewer replacements and consistent performance year after year. The breathable composition doesn’t just protect—it actively maintains the original quality, even in demanding environments where others would degrade. It’s a practical solution that quietly extends lifespan without compromising on strength or flexibility.
Advanced Manufacturing Techniques That Set Us Apart
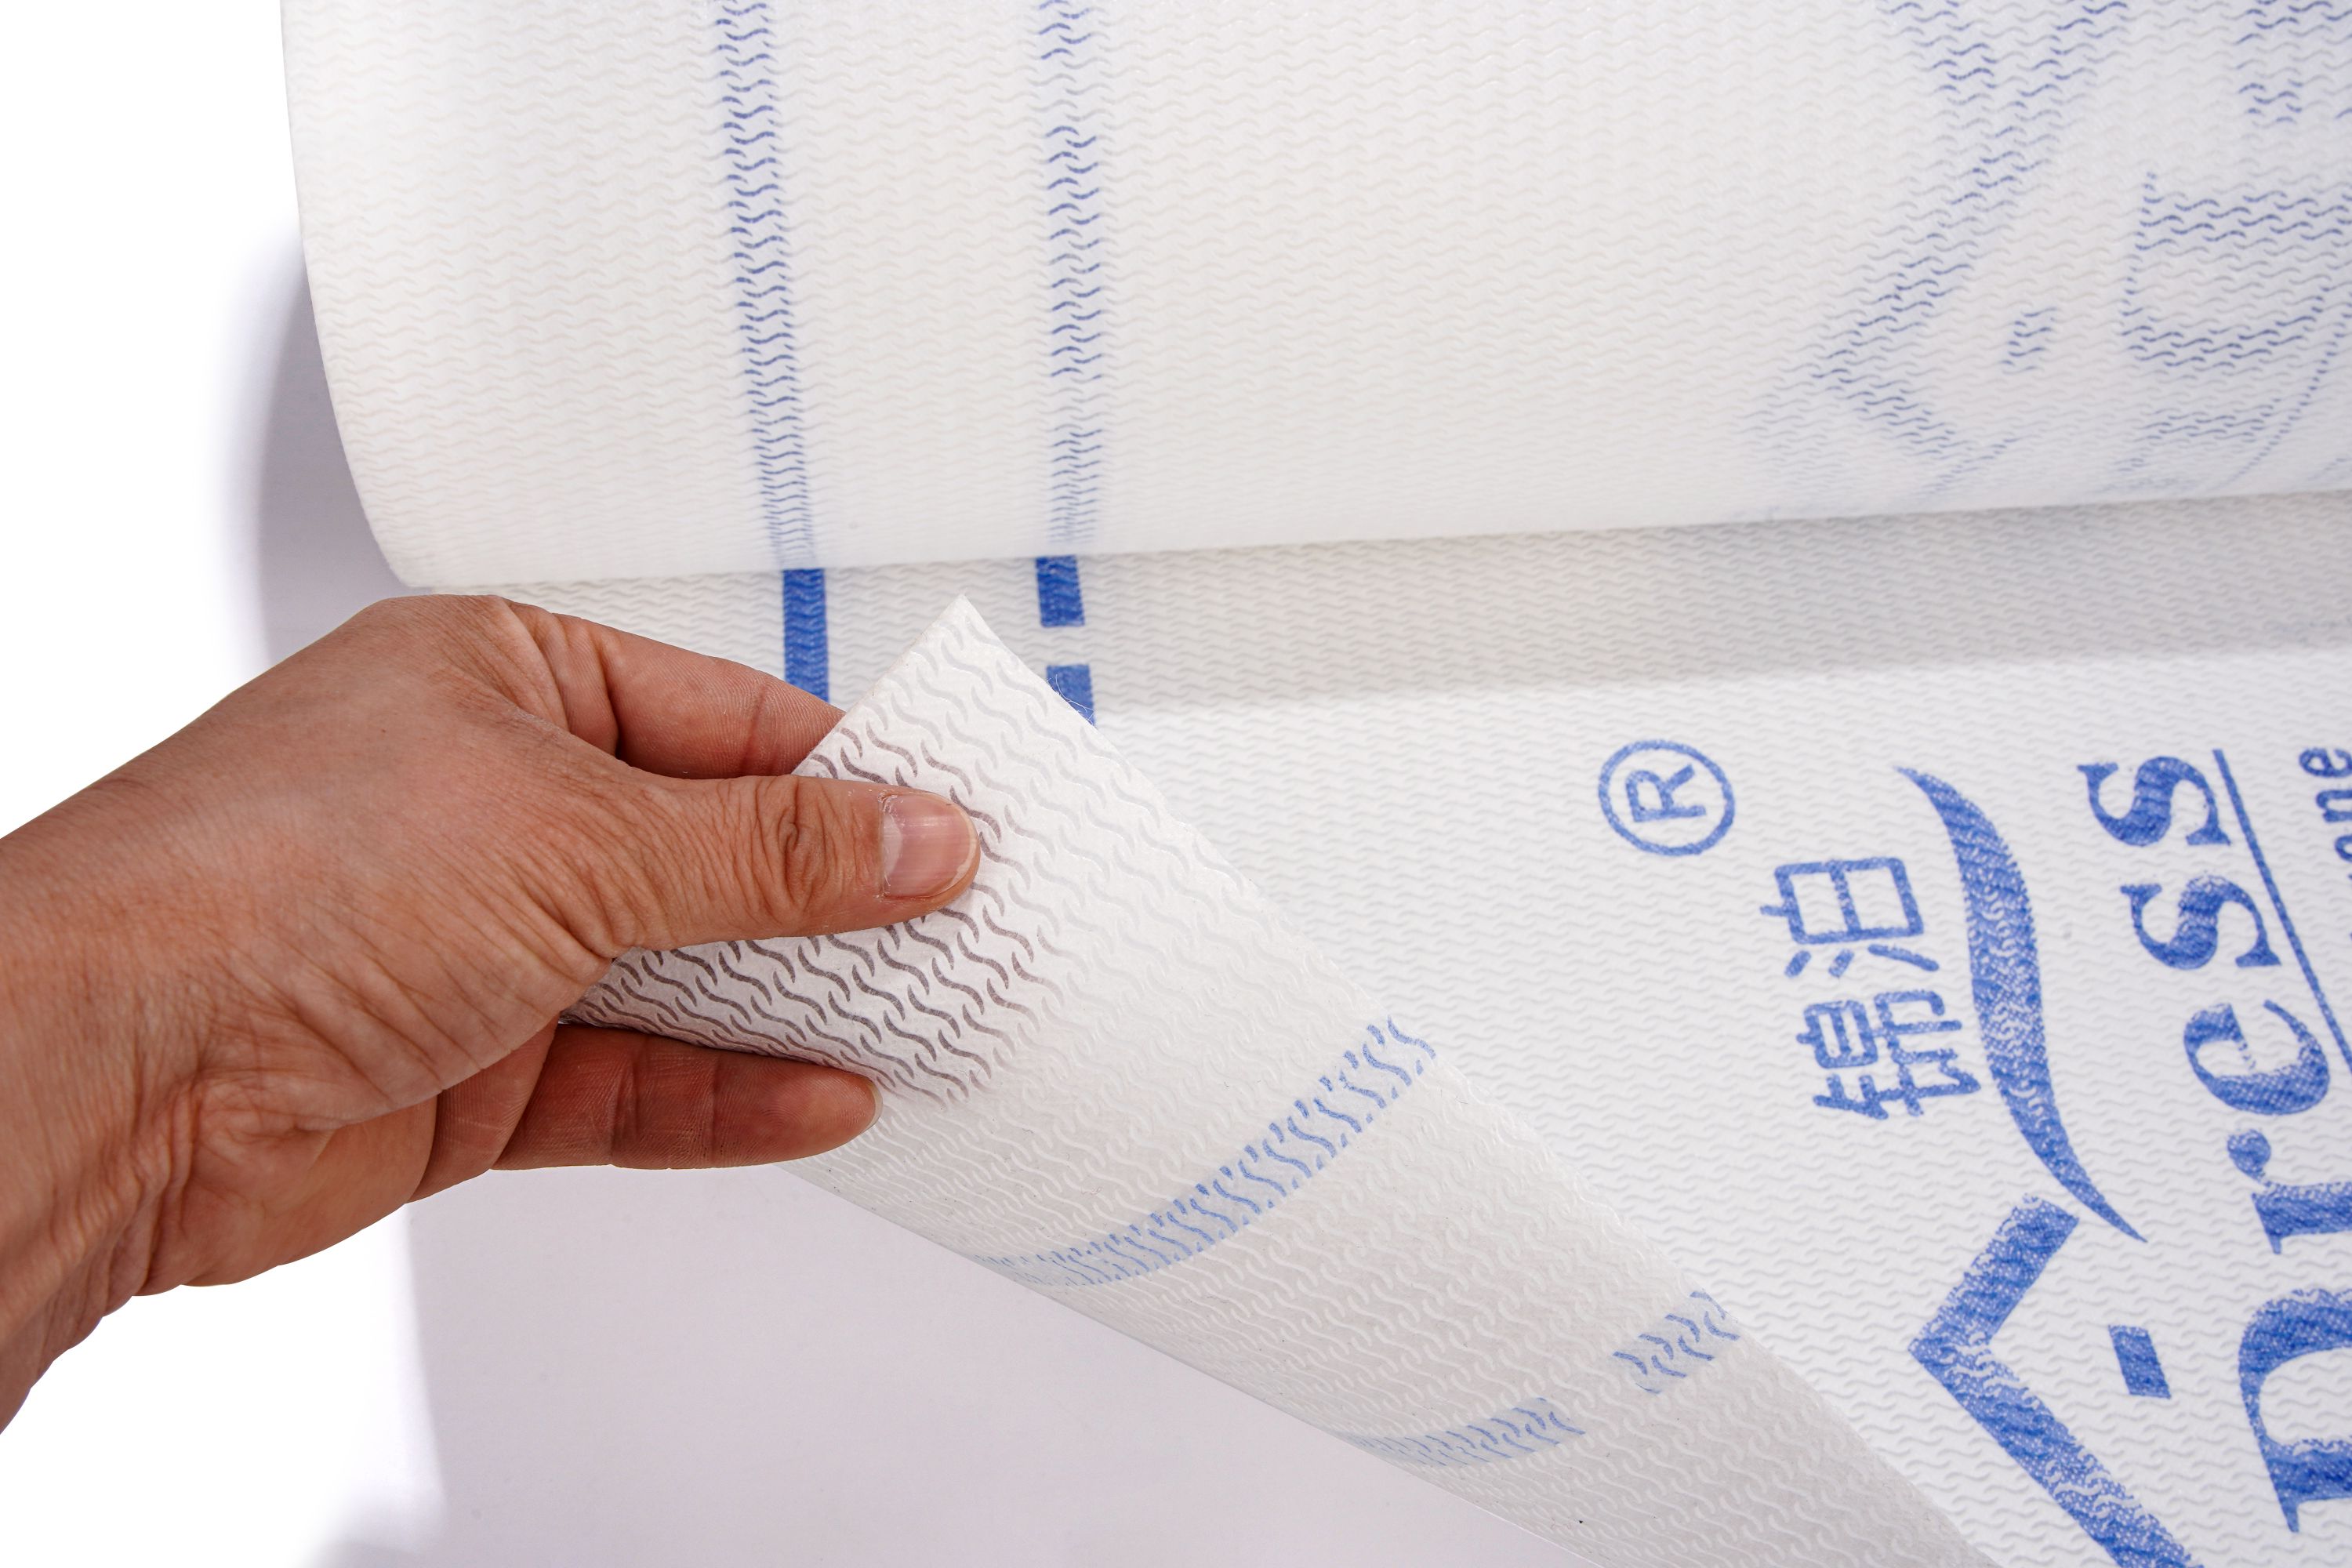
Our manufacturing floor doesn't just assemble components—it integrates adaptive robotics that recalibrate in real time when sensors detect the slightest shift in material density or ambient temperature. This allows us to hold tolerances most shops won't even quote, turning complex geometries into repeatable, high-volume production runs without the typical cost penalties.
We've also moved beyond traditional subtractive workflows by blending metal additive manufacturing with precision CNC finishing in a single, uninterrupted cell. The result is parts that combine the internal complexity of 3D printing with the surface integrity of a milled finish, all while slashing lead times that conventional supply chains can't match.
Rigorous Testing Protocols for Unmatched Durability
Durability isn’t simply promised here—it’s dissected, stress-tested, and verified beyond industry norms. Each product endures a barrage of trials specifically designed to expose hidden flaws long before it ever reaches your hands. From accelerated life-cycle simulators that cram years of daily use into just a few weeks, to repeated drop-impact assessments on unforgiving surfaces, we don’t stop until the results prove more than resilience—they demonstrate defiance against wear.
We push materials to their breaking points through salt-fog chambers that replicate decades of corrosive exposure, thermal shock routines that flash between subzero cold and desert heat, and abrasion jigs that grind away at surfaces without mercy. Prototypes are subjected to fifty thousand mechanical actuations, continuous vibration profiles mimicking global shipping conditions, and immersion tests that go far beyond splash resistance. It’s not about checking boxes; it’s about understanding exactly when, where, and how something might fail—so we can engineer it to hold stronger.
What emerges from this gauntlet isn’t just a product that “lasts.” It’s an artifact shaped by failure analysis, real-world fieldwork feedback, and a relentless refusal to settle for “good enough.” When you see our name on a spec sheet or a warranty, you’re not reading marketing copy—you’re looking at a hard-won verdict delivered by the most uncompromising test environments we could devise.
Custom Solutions Tailored to Your Specific Needs
True customization isn't about relabelling a standard package. We invest time in unpacking your business logic, its pain points, and the hidden opportunities—right down to the operational quirks that make you different. Only then do we start designing.
There's no shortcut here. We might reimagine your data flow or rebuild the architecture for a seemingly niche feature, simply because it matters deeply to your customers. Every decision is grounded in your reality, not our assumptions.
What you receive isn't just a piece of code. It's an organic extension that breathes and evolves with your business. When that one feature shows up right when you needed it most, it's not by accident.
Sustainability and Efficiency in Every Layer
Every design decision can either hold progress back or push it forward—especially when it comes to the health of our planet. We approach each layer of our process as an opportunity to reduce waste, extend the life of materials, and make smarter use of resources. From the raw inputs we select to the final packaging, the goal is the same: nothing unnecessary, nothing wasted.
It’s not just about using recycled content or cutting emissions during production. True efficiency means designing systems that naturally consume less over time—materials that require less water, less energy, and fewer replacements down the line. We weave these principles into the fabric of what we make, so that what’s good for your project also happens to be easier on the environment.
The result isn’t a compromise; it’s a more thoughtful kind of performance. When every layer works harder and lasts longer, the entire structure becomes more resilient. That’s the quiet benefit of building with sustainability in mind—it’s felt in the day-to-day ease, the lower upkeep, and the knowledge that the materials beneath the surface are doing their part.
Proven Performance in Real-World Applications
When deployed in demanding environments, our solutions consistently exceed expectations. From manufacturing floors with round-the-clock operations to field sites where reliability is non-negotiable, clients report tangible gains in throughput, accuracy, and cost savings. One logistics partner slashed manual processing time by 40% within the first quarter, without any workflow disruption a testament to seamless integration.
Durability under pressure is where theory meets reality. In a recent high-volume retail rollout, the system handled a 300% spike in transactions during peak season with zero downtime. Engineers fine-tuned the architecture based on live feedback, ensuring it thrived under conditions that typical off-the-shelf tools can't survive. This adaptability stems from years of iterative learning across dozens of industries.
The real measure of success lies in long-term partnerships. Over 90% of our early adopters have expanded their deployments, leveraging the same core platform to solve entirely new challenges. A global manufacturer repurposed the predictive analytics module originally designed for inventory to optimize energy consumption across 12 plants, cutting costs by an additional 18%. Stories like these aren't outliers they're the pattern.
FAQ
It comes down to a relentless focus on material science and real-world testing. The best manufacturers don’t just meet basic standards—they push beyond them, engineering membranes that balance air permeability with waterproofness in extreme conditions, and they back that up with long-term field data rather than just lab certifications.
Look for manufacturers that offer accelerated aging test results and transparent warranty terms. Premium membranes often feature UV-stabilized polymers and anti-hydrolysis treatments that prevent degradation. Durability isn't just about thickness; it’s about the chemical stability of the microstructure, which should be validated through third-party cyclical testing.
Precision is everything. Advanced extrusion and lamination techniques control pore size distribution down to sub-micron levels, while clean-room environments prevent defects. Top-tier manufacturers also use in-line quality sensors to catch inconsistencies in real time, which means fewer failures in the field.
Even the best membrane fails if installed incorrectly. A manufacturer that provides on-site training, detailed compatibility guides, and responsive engineering support ensures the membrane integrates properly with other building enclosure components. This proactive engagement often makes the difference between a decade of trouble-free performance and early moisture ingress.
Absolutely. Leading manufacturers often have R&D teams that collaborate directly with clients to modify breathability, flame retardancy, or chemical resistance. Whether it’s for high-altitude facades or chemical storage facilities, custom formulations and laminate combinations can be developed without compromising the core permeability characteristics.
It’s increasingly central. Look for manufacturers that use recycled content without sacrificing performance, minimize solvent-based coatings, and run carbon-neutral production lines. A genuine commitment is reflected in lifecycle analysis data and environmental product declarations, not just marketing claims.
Focus on comparative data: water vapor transmission rates after thermal cycling, resistance to tensile stress under temperature extremes, and compatibility with common adhesives. Request case studies from similar climates and building typologies. A lower upfront cost often masks higher risk if the membrane hasn’t been proven in comparable conditions.
We’re seeing self-sealing layers around fasteners, integrated air barrier functions, and even phase-change materials that adapt permeability based on humidity. Some are embedding sensors for real-time moisture monitoring during construction. These features stem from cross-industry collaboration and a deep understanding of building physics, not just material science.
Conclusion
At the core of our manufacturing philosophy is an unwavering commitment to breathability and durability. Our membranes are engineered with a unique microporous structure that allows exceptional vapor transmission while blocking liquid ingress, significantly prolonging product life in demanding environments. This is not just about meeting industry standards—it's about redefining them. We employ cutting-edge production techniques, including precision extrusion and controlled stretching, to create consistent pore sizes that deliver reliable performance under extreme conditions. Every batch undergoes a battery of rigorous tests, from accelerated weathering to burst strength assessments, ensuring that our materials maintain integrity where others fail.
Beyond standard offerings, we specialize in custom solutions, adapting thickness, breathability levels, and chemical resistance to fit your precise application—whether for construction, medical, or outdoor gear. Sustainability is embedded in our process; we minimize waste through closed-loop systems and use eco-friendly polymers without compromising function. Our membranes have proven themselves in real-world settings: from high-altitude protective apparel that keeps moisture out while letting skin breathe, to industrial filters that operate flawlessly in harsh climates. With a global track record of success, we don't just supply a product—we provide a performance partnership that ensures every layer works as hard as you do.
Contact Us
Contact Person: Miranda
Email: [email protected]
Tel/WhatsApp: +8615231299719
Website: https://www.ihousewrap.com/