Abrasive Jumbo Roll Company Selection Guide for Long-Lasting Abrasive Solutions
2026-09-23
A jumbo roll that fails early isn't just a supply problem—it's a production line killer. Yet too many companies choose abrasive jumbo rolls based on price alone, then pay the price in downtime and rework. That's why SHENZHEN SUN ABRASIVES takes a different approach: engineering long-lasting abrasive solutions from the backing up, not just the grit. In this selection guide, we'll walk you through the critical factors to check before you commit to a supplier, so you can say goodbye to premature wear and hello to rolls that actually hold up.
The Real Reason Your Abrasive Rolls Wear Out Too Fast
Most shops assume abrasive rolls fail because the grain dulls. That's rarely the whole story. A far more common culprit is uneven pressure across the contact face. When a roll runs against an idler or workpiece with even slight misalignment, high spots do all the cutting while the rest of the roll skims. Those concentrated zones shed grain quickly, leaving grooves that look like wear but are actually localized overload.
Heat plays a bigger role than people admit. Abrasive rolls aren't designed to store heat. If the backing flexes too much, or the roll is run too fast for the mineral type, the resin bond softens long before the grain is spent. You end up throwing away rolls that still have sharp abrasive, but the bond has glazed or cracked from thermal cycling.
The third hidden factor is clogging. Fine dust from soft metals, wood, or coatings packs into the open coat. Once the surface loads up, friction spikes and the roll starts to tear instead of cut. A roll that wears out too fast is often just running blind. Changing pressure, speed, or cleaning the face will extend life far more than switching to a harder roll.
Supplier Claims vs. What Actually Shows Up on the Pallet
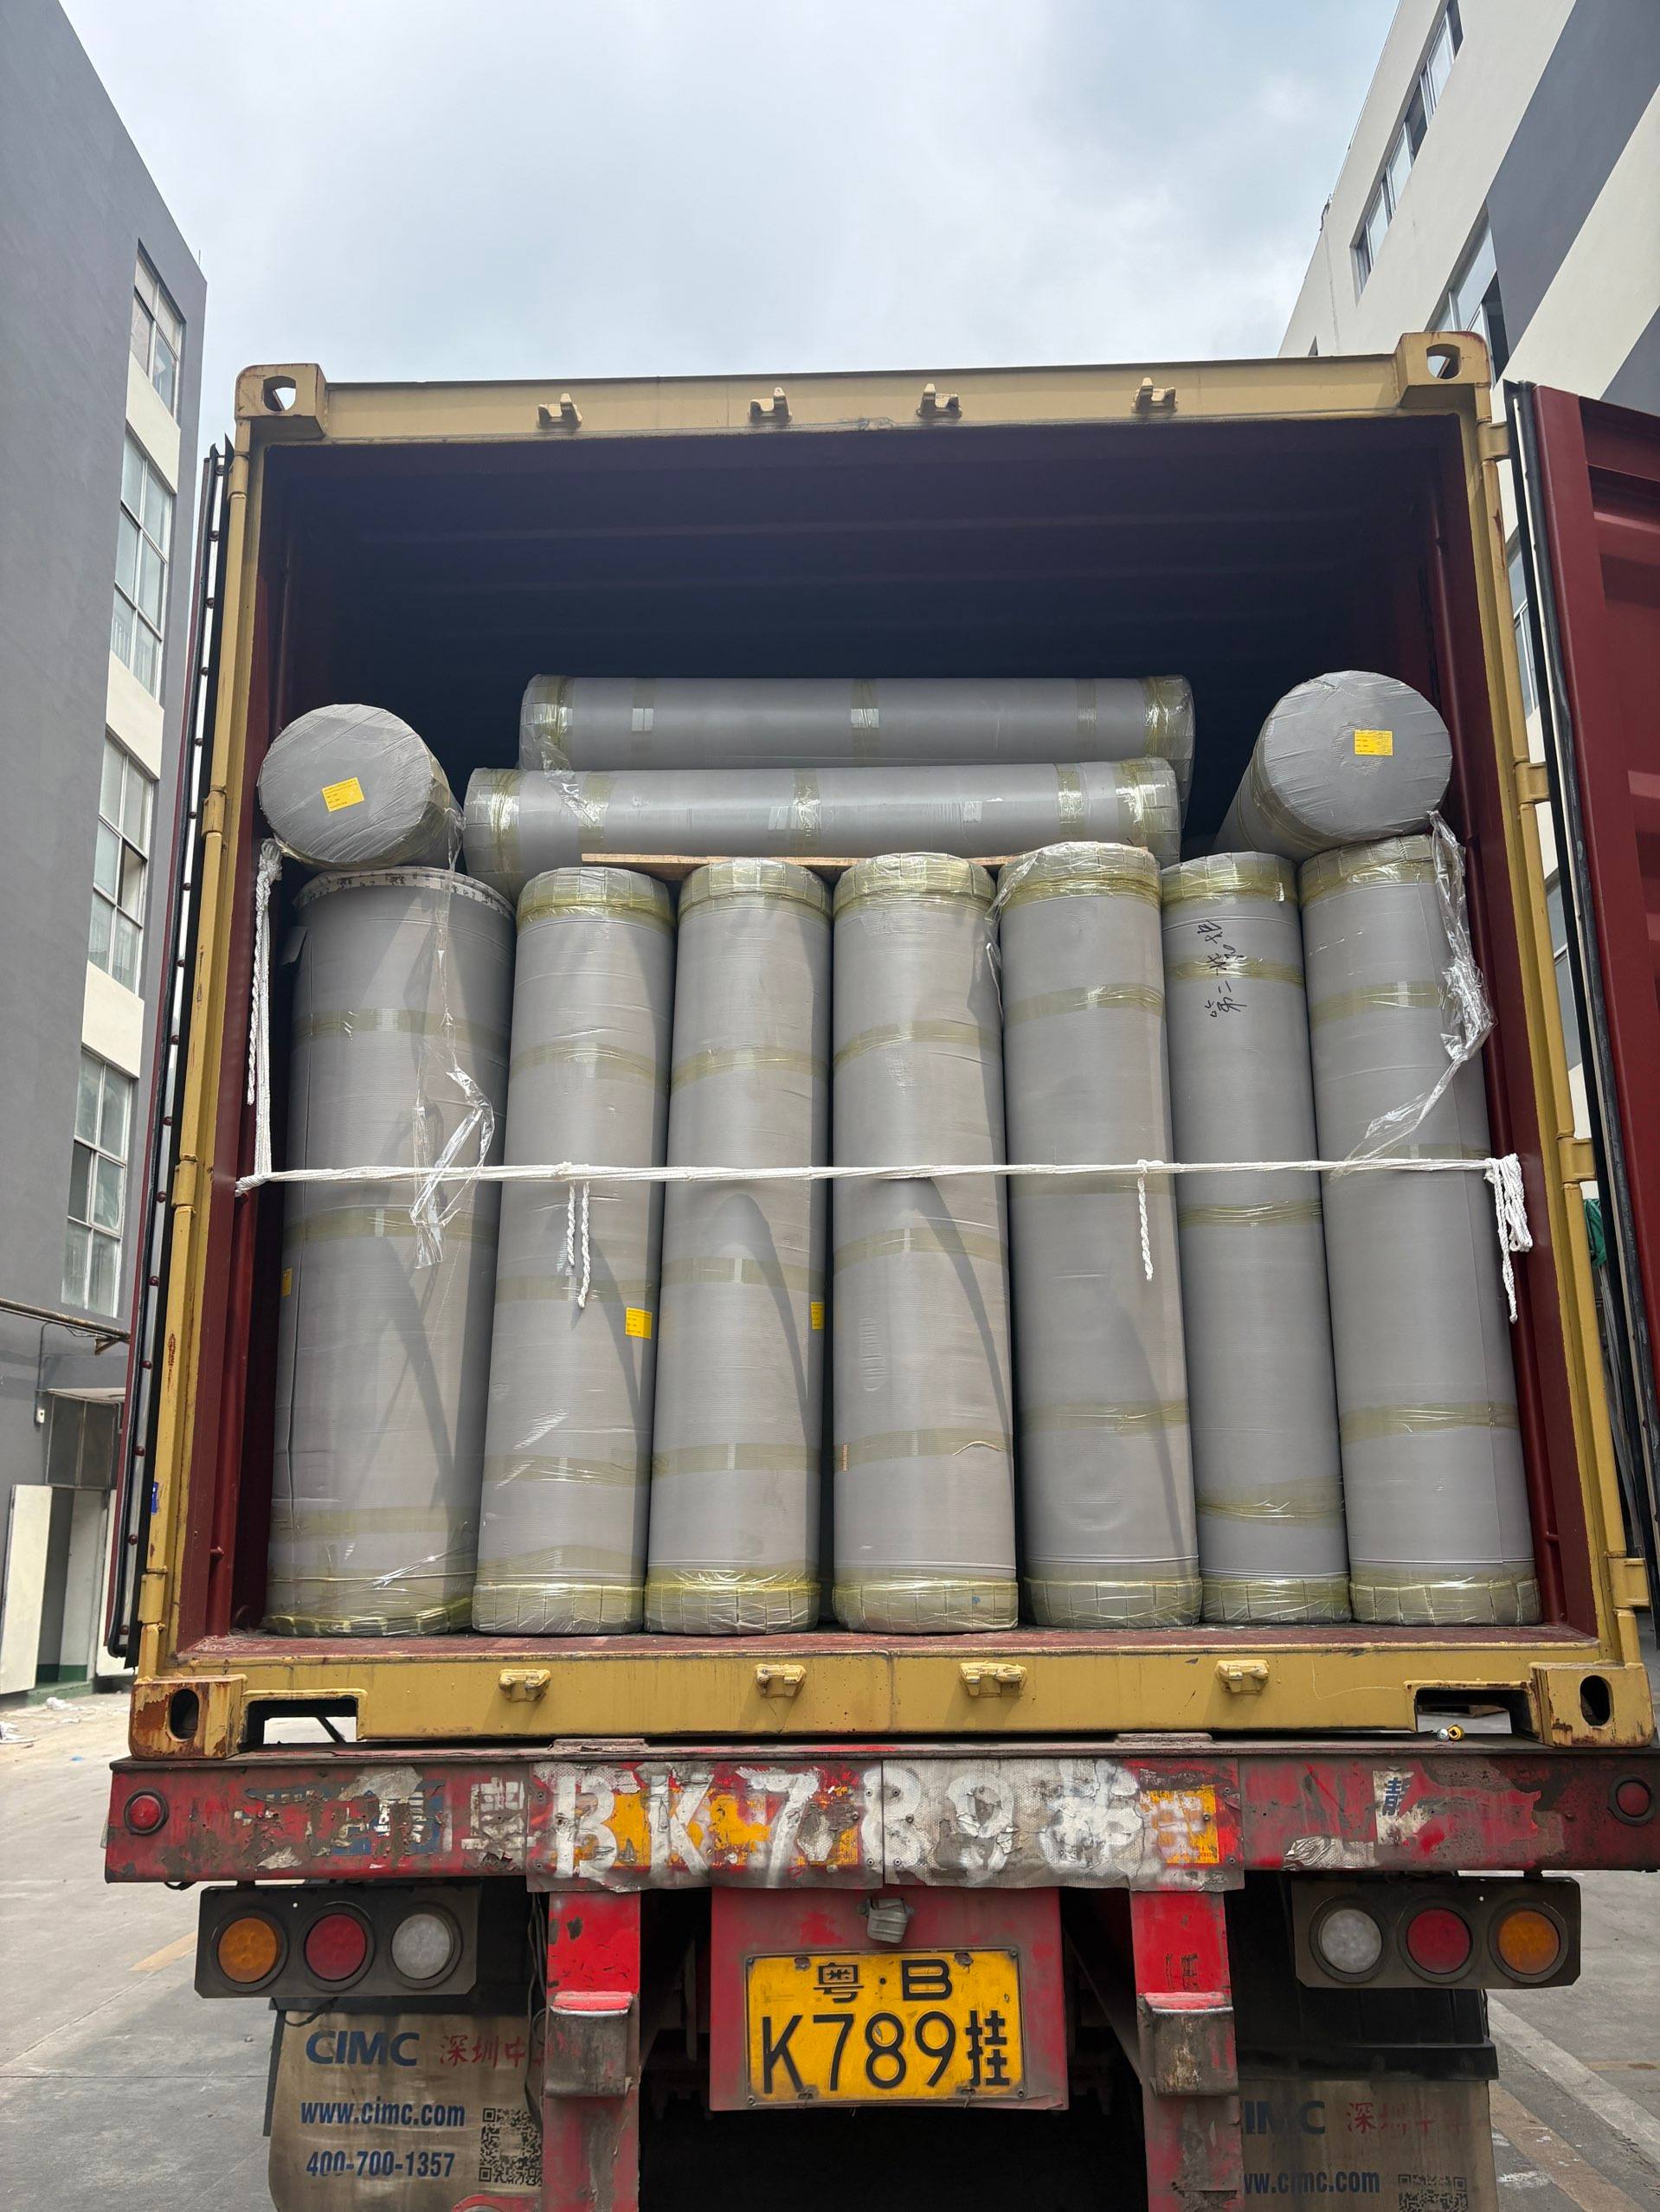
Every warehouse veteran knows the drill: the paperwork says forty cases of 24-ounce jars, but the shrink-wrapped tower in bay three tells a different story. You spot a carton with last season's label peeking through, a hand-scrawled "sub" note half-tucked under the tape, and a row count that only works if some boxes are turned sideways. Supplier claims tend to be optimistic by design—they reflect the order confirmation, not the chaos of a Friday afternoon loading dock.
Once the pallet is broken down, the real inventory emerges in unflattering detail. Mixed lot numbers hide behind a single external SKU, inner packs differ from the master carton markings, and occasionally the count is spot-on but the product inside has been swapped for a slower-moving variant. The gap between claimed and delivered rarely lives in one obvious place; it accumulates across small decisions made upstream—batch merging, partial substitutions, and last-mile repacking that no one flags on the BOL.
That gap costs real money only when it hits the floor. Receiving teams learn to treat supplier manifests as a starting point, not a promise. A quick visual check at the dock, followed by a stratified count of one or two suspect layers, often surfaces more than a full blind audit—because the most expensive discrepancies are usually hiding in plain sight, just waiting for someone to compare the label on the outside with the truth on the inside.
A Jumbo Roll Partner Checklist That Skips the Fluff
Most supplier checklists waste your time with vague promises about “quality” and “service.” What actually matters when you’re sourcing jumbo rolls for converting or high-volume dispensing is whether the partner can hit three hard numbers: core diameter tolerance, roll width consistency, and unwind tension stability. Ask for their last six months of production data on those specs. If they can’t pull that up in an afternoon, move on.
Then look at the physical clues a sample roll gives you. Check for edge dust—run a fingertip along the side and see if it comes away fuzzy. That dust will clog your converting blades or jam dispensers later. Also measure the gap between the paper and the core at three points around the circumference. A gap larger than 4mm means the roll will telescope during transport, no matter how well they wrap it. Finally, ask for a tear-out test on the actual grade you’ll buy, not a lab sheet. The number that matters is wet tensile strength, because most jumbo rolls end up in bathrooms or kitchens where moisture is constant.
Bond Types, Backing Weight, and Other Details That Decide Lifespan
Most people assume every carpet handles foot traffic the same way, but the way fibers are attached makes a huge difference. Woven carpets, especially those made on older looms, hold their shape for decades because the backing and pile are created together as one piece. Tufted styles, which dominate the market today, rely on a secondary backing glued to the primary layer—and that glue is often the first thing to fail. If you notice wrinkles or delamination after a few years, it’s usually not the fiber wearing out but the bond giving up.
Backing weight matters more than the sales tag suggests. A heavier backing doesn’t automatically mean longer life, but it does resist stretching and shifting when furniture moves or kids sprint down the hall. Look for action-bac or woven polypropylene backings with a tight, even weave; cheaper foam backings break down quickly under humidity and heavy use. Also pay attention to pile density and twist—dense, tightly twisted yarns recover better from crushing, while loose, low-density piles flatten permanently within months.
Other quiet factors include latex quality, seam sealing, and even the carpet’s finish. High-quality latex remains flexible for years, while low-grade latex turns brittle and powdery. Seams that aren’t sealed properly unravel at the edges, especially in doorways. And if you pick a carpet with a heavy stain treatment or softener, expect those coatings to wear off unevenly, leaving visible traffic lanes. In short, lifespan isn’t about the fiber alone—it’s about how every layer works together under real daily stress.
When a Lower Price Tag Costs You More in the Long Run
A $30 blender might look like a steal until the motor starts smelling like burnt plastic during your first smoothie. Cheap small appliances are often built around the same weak points: thin plastic gears, non-standard parts, and warranties that vanish after 90 days. You might replace it two or three times in the same period a $90 model would still be running, and each replacement comes with its own trip to the store or delivery wait.
The same pattern shows up in subscription services that lure you in with a $1 introductory price. By month three, the rate jumps to $12, and canceling requires a phone call during business hours. The low starting cost was never the real price, just a way to get your payment details on file. When you add up the sneaky bumps and time spent opting out, a straightforward competitor with a higher upfront fee often ends up cheaper.
Cost per use is the real scoreboard. A $20 backpack whose zipper splits on the second commute costs $10 per trip before it fails; a $120 bag that survives five years of daily abuse comes to pennies per day. Factor in the hassle of returns, replacing your stuff, and the landfill guilt, and the bargain aisle starts to look like a tax on people who can't afford to buy things twice.
Locking in a Supplier Who Can Keep Up With Your Toughest Jobs
Most suppliers look great on paper until you hand them a job with tight tolerances, a short turnaround, and zero room for error. Then the cracks start to show: missed calls, vague timelines, and a sudden reluctance to commit. That’s why locking in the right supplier isn’t just about checking boxes on a vendor form. It’s about running them through a real test—one that mimics the pressure of your hardest projects. Ask for a sample run on your most demanding spec, not their standard showcase piece. Watch how they handle a change order at the eleventh hour. Pay attention to whether they ask the uncomfortable questions upfront or wait until something breaks.
A supplier who can keep up with your toughest jobs does more than deliver on time. They flag risks before you see them, bring alternative materials when lead times shift, and never make you chase them for a status update. You’ll know you’ve found the right one when the conversation shifts from price per unit to how they plan to solve your next headache. Don’t settle for a vendor who needs hand-holding. Lock in the one who treats your hard jobs as their own.
FAQ
Look for a supplier that shares detailed batch test reports, including grain adhesion strength and backing tension limits. If they hesitate to provide those numbers, their rolls likely won't hold up under continuous use.
Ceramic alumina grains self-sharpen under heat and pressure, making them ideal for stainless steel or titanium. Zirconia alumina resists dulling on carbon steel, while aluminum oxide is more budget-friendly but wears faster on tough alloys.
A cotton or blended polyester backing bends without cracking, letting the abrasive follow curves and corners. Rigid paper or fiber backings tend to snap or tear on edges, which shortens the roll's usable life and leaves uneven finishes.
Yes. If edges are trimmed unevenly or the roll wanders during slitting, you'll see tracking problems on wide belt sanders. That causes premature edge wear and forces more frequent roll changes, which quietly eats into your throughput.
Request details on the resin system and cure cycle. A two-stage phenolic resin with a controlled post-cure bake usually gives stronger grain retention than a single-stage bond, especially when grinding with high pressure or fast belt speeds.
Moisture absorption in the backing or bond can weaken the adhesive layers and cause curling or grain loss. A reliable supplier will store rolls in climate-controlled conditions and ship them in sealed, moisture-resistant packaging.
Tight slitting tolerances mean each cut strip stays within a few thousandths of an inch, so you don't waste material on overlapping or gaps. Cheaper rolls often have wider tolerances, leading to frequent jams or uneven wear on your equipment.
They ask about your workpiece material, contact pressure, belt speed, and coolant use before recommending a roll. Then they offer a trial strip or sample batch to validate performance rather than pushing the highest-priced option.
Conclusion
Look past the glossy brochures and you will find the same story in most shops: abrasive rolls that lose their bite halfway through a shift. The culprit is rarely the operator. More often, it is a supplier cutting corners on grain concentration or using a backing that stretches under pressure. Ask for a roll sample before committing and run it on your worst surface, not a clean test coupon. A supplier who hesitates to send a trial roll is already telling you what will arrive on the pallet later. The checklist that matters is not about certifications or warehouse size. It is about consistent grain spacing, edge-to-edge coating weight, and a splice that does not thump. If the sales rep cannot answer those three things without flipping through a catalog, keep looking.
Bond type and backing weight decide whether a roll lasts weeks or days. Resin-over-resin bonds hold up on high-speed steel, while lighter backings tear when you lean into a weld. Cheaper rolls often skimp on both, so the per-roll price looks great until you are changing rolls three times a day. That labor and downtime dwarfs any upfront savings. The right partner will not push you toward the cheapest option. They will ask about your substrates, pressure, and speed, then recommend a roll that can survive your toughest jobs without ballooning costs. Lock in a supplier who stocks the full weight range and can ship replacements fast, because a roll that is backordered is a roll that is costing you money.
Contact Us
Contact Person: Amanda Wang
Email: [email protected]
Tel/WhatsApp: +86-13602569854
Website: https://www.sunabrasives.com.cn